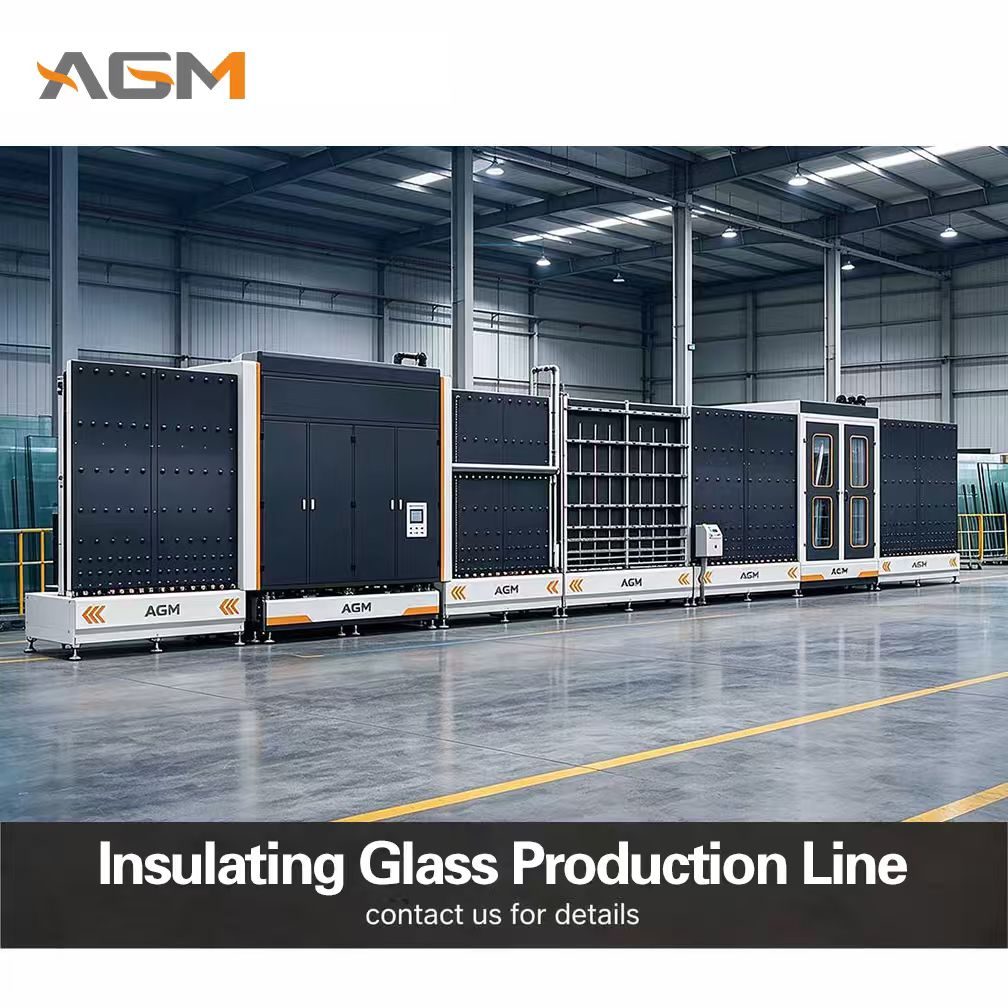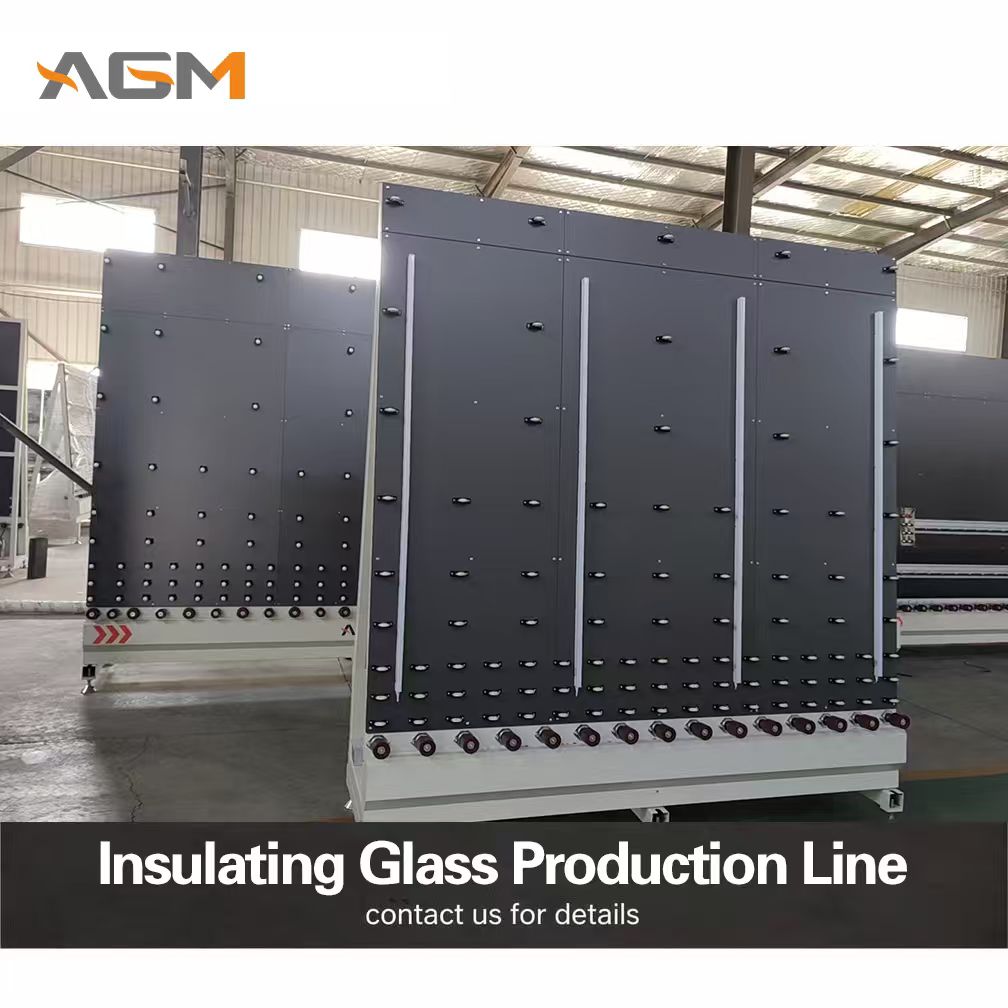
Choosing an insulating glass production line is a sequencing problem, not a budget problem. Fix the glass mix first, then real shift output, then station cycle times, and compare prices only after one specification sheet is locked.
Most buying mistakes come from the order of the questions, not from the answers. Buyers who open with “how much” end up comparing machines that were never configured for the same job.
Start with your glass mix, not the price list
Glass mix decides which configuration is eligible before any commercial discussion starts. Double glazing, triple glazing, stepped units and large-format units each add or remove stations.
Write down the mix you expect to run in the first two years, as a share of square meters. Include cavity width and spacer type. Then check what each element changes on the line:
| Your glass mix | What it changes on the line | Ask the supplier to confirm |
|---|---|---|
| Double glazing only | One press cycle per unit, fewer handling steps | Rated range at your size |
| Triple glazing | Two cavities, longer cycle per unit | One pass or two for two cavities |
| Stepped or shaped units | Off-line positioning and sealing work | Which stations accept stepped edges |
| Large-format units | Table size, suction cups, tilt or crane handling | Table size and unit weight |
| Low-E coated glass | Coating-side detection, edge deletion if required | In-line or off-line edge deletion |
| Warm edge spacer | Spacer bending and butyl application change | Whether the bending head covers your profile |
A mix that is 90% double glazing with one cavity width does not need the same line as a mix with weekly triple-glazed and stepped orders. The second mix pays for stations the first mix never uses.
Every mix is then checked against hard limits. The line described in this guide is rated as follows:
| Rated parameter | Value | What it constrains |
|---|---|---|
| Glass thickness | 3–12 mm | Which pane sets the line can run; a pane set outside this range needs a different specification |
| Maximum unit size | 2500 × 3600 mm | Large-format orders; anything above that size cannot run on this line |
| Power supply | 380 V / 50 Hz | Site supply and any transformer; a mismatch is a delivery problem, not an installation problem |
| Conformity | CE marked | Market access; request the declaration of conformity and the directives applied |
What an insulating glass production line actually consists of
The line itself is a set of connected stations that wash, frame, fill, assemble and seal panes into one sealed unit. Output is set by the slowest station, not by the longest machine.
A line built around manual frame placement runs a different sequence from a line with an in-line spacer bender. This is the sequence most mid-size plants run:
- Washing and drying: three pairs of brushes, purified water, single or double air knife. Defects that surface years later usually start here, as covered in why glass washing decides seal life.
- Inspection and framing: inspection light, then aluminum frames placed by hand.
- Press section: the panes meet here; the closing method is covered below.
- Gas filling (optional): argon through ports in the press base during closing.
- Loader: conveyor wheels, single panes only.
- Unloader: V-belt groove keeps sealant off the belt; finished units only.
Water quality belongs in this list, not in the maintenance manual. Mineral-heavy water attacks machine components and leaves drying marks that appear only after the unit is already sealed. Washer access matters for the same reason: double doors let the brush and air-knife area be cleaned without dismantling the line.
Inner closing or outer closing: pick by glass size, not by habit
Inner closing holds large panes by suction inside the press until the second pane arrives; outer closing is faster because both panes enter before the press closes.
The two methods produce the same unit. They differ in what happens if a pane slips, and in how much time each cycle takes. For a plant running heavy large-format units, the slower method is the cheaper one. For a plant running small units at volume, the faster method wins.
| Option | How it works | Where it wins |
|---|---|---|
| Inner closing | First pane held by suction, second joins, then press closes | Large panes at risk of dropping |
| Outer closing | Both panes enter before the press closes | Speed on small and medium units |
| Triple glazing, one cavity per pass | Press, return, press the second cavity | Lower machine cost, more handling |
| Triple glazing, two cavities per pass | Both cavities pressed in one pass | Fewer handling steps on triple orders |
| Argon during press | Gas through press base ports while closing | No separate gas station |
| Dual sealant supply | Silicone and polysulfide fed separately | Two sealants, no purging between runs |
Two lines with identical table sizes can differ by a wide margin in shift output, because the bottleneck sits in a different station. That is why cycle time, not table size, belongs in the comparison.
Calculate real output, not nameplate speed
Shift output equals cycle time at your dominant size, multiplied by usable hours, minus changeover and rejects. Nameplate speed describes one station running one size and rarely survives a mixed order book.
Apply three corrections before you accept any capacity figure:
- Use the size band that dominates your orders, not the maximum table size.
- Subtract changeover for every product change: spacer, cavity width, glass thickness.
- Subtract rework: washing rejects, gas failures and seal rework all consume cycle time.
Then ask for cycle time at that size in writing, together with the changeover minutes the supplier assumed. Two quotations that both claim the same daily output can differ substantially once these two numbers are put side by side. The method is set out in how to calculate real IG line capacity.
Specify utilities and voltage for your market
Utilities are confirmed last and regretted first. Air quality, water quality, power configuration and floor loading cannot be upgraded after installation without stopping production.
State all five in the inquiry, not after the order:
- Compressed air: dry, oil-free, stable pressure at the sealing station.
- Water: spot-free rinse; water quality shows up as marks after drying.
- Power: destination market, voltage, frequency and phase; the line described here is built for 380 V / 50 Hz, so any other supply has to be agreed before the order, not after delivery.
- Floor and access: line length, turning space for long units, floor flatness.
- Climate: ambient temperature affects sealant cure and gas retention checks.
Compliance is two separate questions. The first is the machine’s own conformity route for the destination market; the line described here is CE marked, and the declaration of conformity plus the list of directives should travel with the quotation. The second is the product standard your sealed units must meet, such as EN 1279 in Europe or ASTM E2190 in North America. Ask which documents the supplier provides and which ones the buyer must obtain locally.
The plant layout decision — floor space against handling method — is covered in vertical vs horizontal insulating glass line.
Five specification mistakes buyers make
Most specification errors are omissions, not wrong choices. The buyer orders a line without stating the constraint that later limits it, and the gap appears at commissioning.
| Mistake | What it costs | How to avoid it |
|---|---|---|
| Sizing on maximum unit size | Paying for table capacity the order book never uses | Size on your dominant band |
| Comparing on nameplate speed | Two quotes that cannot be compared at all | Require cycle time at a named size, in writing |
| Omitting thickness range and coating type | Stations specified for the wrong glass | Give minimum and maximum thickness plus coating side |
| Leaving out destination voltage and frequency | Transformer or motor change after delivery | Put market and supply data in the first inquiry |
| No written acceptance test | Disputes at handover | Define output and seal checks before the order |
A sixth mistake sits outside the machine: assuming the line will be run by the same team that installed it. Ask who trains the operators, for how many days, and whether training happens on production orders or on samples.
Get comparable quotes before comparing prices
Two quotations are comparable only when they describe the same stations, the same cycle times at the same size, and the same scope of installation and training. Comparing price before that is a comparison of documents, not of machines.
Ask every supplier for the same five items: station list with cycle times, included and excluded scope, recommended spare parts, commissioning and training days, and warranty terms in writing. A quotation that cannot answer these five is not cheaper; it is unfinished. The full inquiry checklist is in what to send before requesting an IG line quotation.
FAQ
What is an insulating glass production line?
An insulating glass production line is a connected set of machines that wash, frame, fill, assemble and seal two or more panes into a single unit with a desiccant-filled cavity.
What glass thickness can an insulating glass line process?
The rated thickness range is a machine specification, not an industry standard. On the line described in this guide it is 3–12 mm. Ask for the written range at the size you actually run, including coating type and total unit thickness.
Does a bigger line produce more square meters per shift?
No. Throughput follows cycle time and usable hours, while a larger table only raises the maximum unit size. A large line fed with small orders can produce less than a smaller line built for that order pattern.
How long does it take to install and commission?
It depends on line length, site readiness and whether commissioning includes trial production. Ask for a schedule with milestones: arrival, mechanical completion, utilities connection, first sealed unit, acceptance test.
Key takeaways
- Choose in this order: glass mix, real shift output, station cycle times, utilities, then price.
- The slowest station sets output, so compare cycle times rather than nameplate speeds.
- State destination voltage, frequency and floor conditions in the inquiry, not after delivery.
- Two quotes become comparable only when station lists and cycle times match.
Send the glass mix you expect to run, the size band that dominates your orders, and the shift output you need. That is enough to map the requirement onto an insulating glass production line configuration and to state the station cycle times that set its output.